A solid-state electrode coating R2R line is a continuous process that applies sulfide-based solid electrolyte onto a current collector using a slot-die method. Domestic electrode-process equipment maker CIS has built a continuous sulfide-based solid electrolyte pilot line at its Daegu Plant 3, with an annual production capacity of 2–5 tons. Compared to wet slurry, sulfide electrolyte is highly moisture-sensitive, requiring simultaneous management of roll-surface contact time and tension deviation. This is where a mechanical contradiction arises: lowering tension increases weaving, while raising tension increases the risk of web breakage and electrolyte powder shedding.
Within how many newtons must tension deviation be controlled to satisfy the coating thickness tolerance? Through this pilot line, CIS stated it expanded its sulfide-based solid-electrolyte production capacity from an existing 840 kg/year to a 2–5 ton/year scale, and as of July 2025 it began supplying samples to OEMs and North American solid-state battery developers (Source: THE ELEC, Hankyung 2026-02-26).
Kinematic Analysis
The tension roll system consists of a tension-transfer path across three sections: the unwinder, the coating section, and the rewinder. The tension difference across each section is determined by the sum of roller inertia and bearing friction torque. The dancer roll just before the coating section is a buffering element that absorbs tension fluctuations, with its spring constant and dancer travel governing response speed. From a load-path perspective, deflection of the dancer roll shaft directly translates into tension deviation, making shaft stiffness a top-level design variable for coating thickness uniformity. The dancer-roll spring constant is designed per KS B 2400 (Design Standard for Compression and Tension Cylindrical Coil Springs), and domestic registered patent KR101000826B1 presents a pendulum-dancer tension control method for high-speed R2R systems that can serve as a reference for dancer response-speed design.
Calculation/Formula Verification
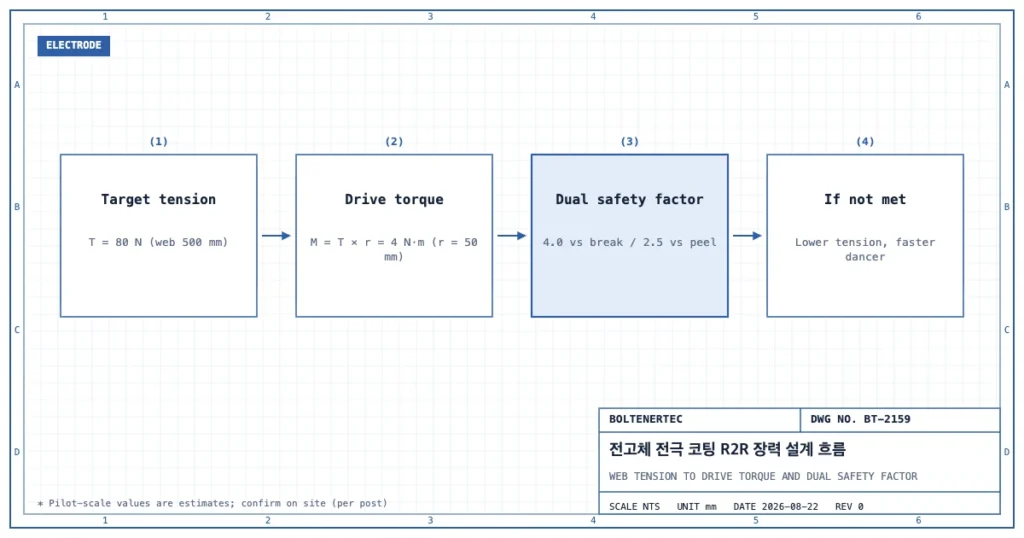
In the relationship between web tension $T$ (N) and roller radius $r$ (mm), the drive torque is as follows.
$$M = T \times r \times 10^{-3}$$
Here $M$ is in N·m. Applying a web width of 500mm, target tension of 80N, and tension-roll radius of 50mm (estimated: typical specification for a pilot-scale R2R line, on-site measurement and reconfirmation required) gives $M = 80 \times 0.05 = 4$N·m. This value must be reverified by converting it to the instantaneous tensile stress the web experiences immediately after coating. Safety factor is applied twofold: a first factor of 4.0 or higher against web breaking strength, and a second factor of 2.5 or higher against coating-layer peel strength. If both criteria cannot be satisfied simultaneously, the design must shift toward lowering tension and increasing dancer roll response speed to correct weaving. The dancer-roll response delay time $\tau$ can be approximated as the ratio of spring constant $k$ (N/mm) to dancer moving mass $m$ (kg), i.e. $\tau \approx 2\pi\sqrt{m/k}$ (estimated: a first-order approximation; actual response varies with bearing friction and pneumatic damping, so on-site measurement and reverification are required). This approximation only indicates the design direction that the dancer’s natural frequency must be sufficiently higher than the line-speed variation frequency for weaving correction to occur without delay; the exact $k$ value must be reverified against the spring manufacturer’s specification sheet per the KS B 2400 standard.
Shop-notes
For the tension roll surface, ceramic coating is considered as the primary option over hard chrome plating to prevent sulfide powder adhesion. Ceramic coating requires securing at least 0.05mm of post-machining grinding allowance to meet roundness tolerance, so the grinding allowance must be separately marked on the machining drawing (machinability note). A non-contact air-turn roll was considered as an alternative but not adopted. The reason it was not adopted is that the burden of maintaining line cleanliness under dust scattering is greater than with a contact-type roll. Tension-roll drive motor capacity requires on-site measurement and reconfirmation. In Korea, KOSDAQ-listed electrode-equipment specialist CIS has leveraged its wet-electrode equipment technology to secure dry-coater mass-production capability while also pursuing solid-state materials and equipment commercialization, suggesting that domestic tension-roll designs should likewise shift toward surface-treatment and tolerance-management schemes that reflect higher dust sensitivity than wet processes (Source: Hankyung, 2026-02-26).
Design Reflection Checklist
- Has the tension deviation control value been calculated and dual safety-factor verification completed?
- Has the dancer roll spring constant been measured on-site?
- Has the tension roll surface treatment’s grinding allowance been reflected in the drawing?
- Has the drive motor capacity been reconfirmed on-site?
- Whether the dancer-roll response-delay approximation has been compared against the line-speed variation frequency
- Whether the pilot-line specification reflects the expanded solid-electrolyte capacity (2–5 t/year class)
One-Line Summary
For a sulfide-based solid-state electrode coating R2R line, tension deviation control is a design variable that takes precedence over coating thickness tolerance.