Dry-electrode R2R equipment investments in the US and Europe were announced in the same week. On August 19, 2026, Forge Nano (US) held a groundbreaking ceremony for a battery manufacturing facility in Morrisville, North Carolina, with manufacturing equipment to be brought in sequentially over the next two years as part of a defense supply-chain strengthening effort. In Europe, Germany’s UniverCell announced it raised EUR 30 million to expand lithium-ion cell production based on dry-coating technology; as of its April 2026 progress update, dry cathode extrusion, R2R coating/UV curing, and R2R lithium-metal deposition processes have all been converted to pilot scale.
According to Forge Nano’s own announcement (IR press release, August 19, 2026), the expansion is backed by up to USD 100 million in non-dilutive funding from the U.S. Department of Energy (DOE) and a USD 20 million strategic investment from Samsung SDI (USD 10 million in Series D financing, USD 10 million in PIPE financing) (source: Forge Nano IR). The facility will expand from roughly 100,000 to approximately 315,000 square feet, with a planned capacity at full production of up to 3 GWh annually and around 150 million cells per year (same source). The production-start target is 2028, timed to align with U.S. National Defense Authorization Act (NDAA) requirements taking effect that year (same source). According to UniverCell’s own material (Tech.eu, March 5, 2026), the company operates a gigafactory in Northern Germany with scalable capacity beyond 1.5 GWh and manufactures custom 21700 cylindrical tabless cells in-house (source: Tech.eu).
Mechanical-Design Impact Analysis
The dry-electrode process eliminates the drying oven because there is no slurry solvent, but rolling load in the extrusion/calendering section increases instead. Where the wet slot-die line’s design variables were tension and drying temperature, the dry line’s design variables are roll-gap rigidity and dust-scatter control. In a dusty environment, dust-explosion prevention equipment (dust collection, grounding, explosion-proof rating) under Korea’s Occupational Safety and Health Act must be reflected from the initial enclosure design stage of the rolling section — reflecting this early lowers the likelihood of an ECO compared with a later retrofit.
Because roll gap directly reflects dry-film thickness deviation, crown compensation design to suppress roll-shaft deflection becomes more important than in the wet process. Since the US approach centers on defense supply-chain security and the European approach centers on R2R process maturity, the priority of requirements at equipment order time is likely to differ between the two. Control/software-based process monitoring is referenced here only as a boundary condition for this design.
Converting Forge Nano’s 3 GWh / 150-million-cell target into an annual operating-day basis works out to roughly 5 cells produced per second, implying that the dry-electrode line’s calendering and slitting speed must be designed so it does not become a bottleneck relative to wet processes. UniverCell’s production of 21700 cylindrical tabless cells means applying dry-electrode film to cylindrical winding, which likely requires a winding tension profile designed separately from flat pouch/prismatic formats to account for the dry film’s lower flexibility (estimated; exact winding parameters undisclosed).
Shop-notes: When winding dry-electrode film into a cylindrical format, options include a lower-cost approach that reuses the existing winder’s tension-roller layout designed for wet film, versus a higher-cost approach that fully replaces the rollers with low-friction, static-control rollers dedicated to dry film. The former has lower retrofit cost but retains crack/delamination risk from the dry film’s lower flexibility, while the latter requires greater investment but is more favorable for securing mass-production yield on cylindrical cells — likely the more rational choice given a target of 150 million cells (estimated).
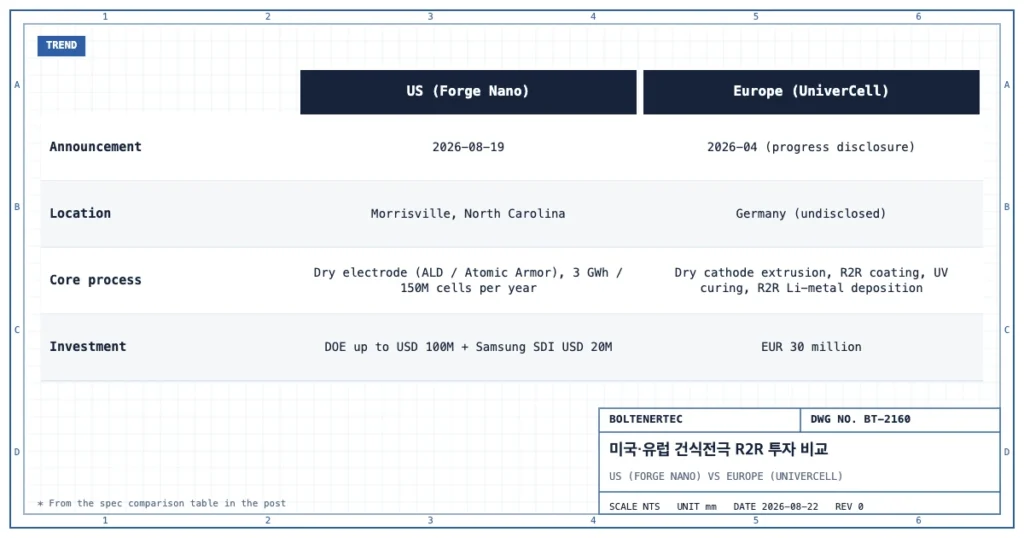
Spec Comparison Table
| Category | US (Forge Nano) | Europe (UniverCell) |
|---|---|---|
| Announcement date | 2026-08-19 | 2026-04 (progress disclosure) |
| Location | Morrisville, North Carolina | Germany (undisclosed) |
| Core process | Dry electrode (ALD / Atomic Armor coating tech), 3 GWh / 150M cells per year target (production start 2028) | Dry cathode extrusion, R2R coating, UV curing, R2R Li-metal deposition |
| Investment scale | DOE non-dilutive funding up to USD 100 million + Samsung SDI USD 20 million | EUR 30 million |
| Equipment install schedule | Sequential over next 2 years (undisclosed) | — |
One-line summary: The US is pushing electrode equipment investment along a supply-chain security axis, while Europe pushes along a dry R2R process-maturity axis — both axes are variables that must be reflected in domestic equipment export spec-response strategy.
Design Reflection Checklist
- Review whether low-friction, static-control rollers are needed for cylindrical winding of dry-electrode film
- Pre-simulate whether calendering/slitting line speed becomes a bottleneck against the 3 GWh / 150M-cell throughput target
- Incorporate dust-explosion prevention equipment (dust collection, grounding, explosion-proof rating) from the earliest enclosure design stage