Samsung SDI’s registered patent KR101156266B1 claims a structure that reinforces the weld joint between a battery cell and connecting tab with an anisotropic conductive film (ACF). This is a patent with implications for connecting-tab forming equipment.
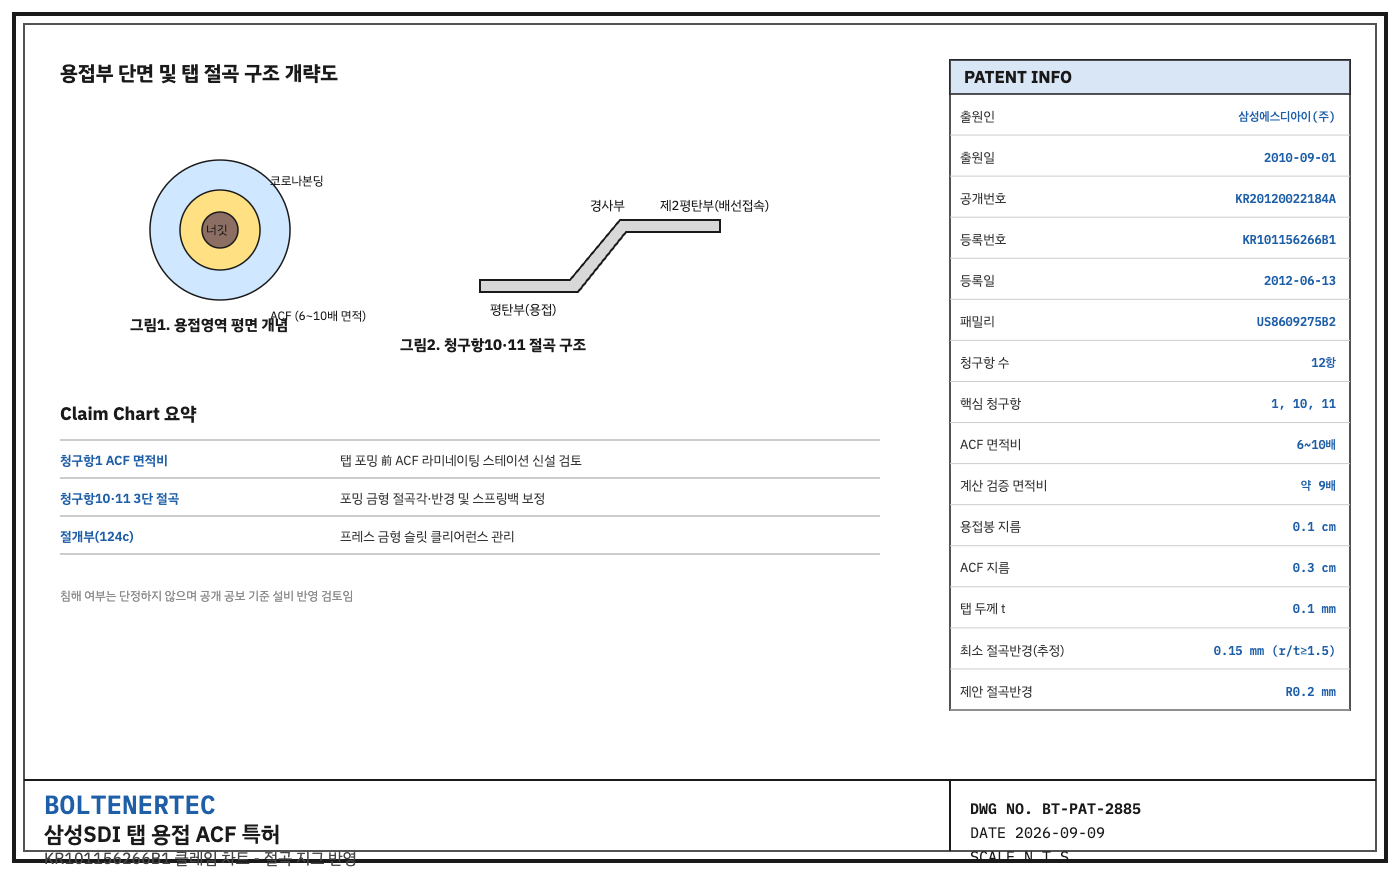
Bibliographic Information
| Item | Content |
|---|---|
| Applicant | Samsung SDI Co., Ltd. |
| Filing Date / Priority Date | 2010-09-01 |
| Publication No. / Date | KR20120022184A / 2012-03-12 |
| Registration No. / Date | KR101156266B1 / 2012-06-13 |
| Family | US8609275B2 (priority claimed 2011-05-18) |
| Invention Title | Battery Pack (BATTERY PACK) |
Key Claims Summary
Claim 1 claims a battery pack structure in which an anisotropic conductive film (ACF), with an area larger than the weld area, is formed around the periphery of the weld area between the battery cell and connecting tab, bonding the two together. The specification states that an ACF area of 6–10 times the weld-area size balances adhesion improvement against cost. Claims 10 and 11 specify that the connecting tab has a three-stage bend structure consisting of a flat section corresponding to the weld area, an upward-bent inclined section, and a second flat section for wiring connection.
Claim Chart: Claim Elements vs. Equipment Reflection Review
| Claim Element | Patent Content | Equipment Element from boltenertec’s Perspective |
|---|---|---|
| Weld area (nugget + corona bonding) | Trace of resistance-welding electrode current, elliptical formation | Design criteria for tab-welder electrode tip shape and applied-pressure profile |
| Anisotropic conductive film (ACF), area ratio 6–10x | Dual mechanical/electrical bonding via ACF around the weld periphery | Whether to add an ACF laminating process before tab forming; review of impact on line tact time |
| Connecting-tab flat section–inclined section–second flat section (Claims 10, 11) | Three-stage bend separating the weld area from the wiring connection point | Tab-forming die bend-angle and bend-radius design, springback compensation |
| Cutout (124c) | Reduced second-region width for easier bending | Press-die slit clearance, burr management |
Calculation Verification for Equipment Reflection
To avoid fracture when forming the bend area, the bend radius r must be at least a certain ratio of the sheet thickness t. Because the minimum bend-radius ratio for nickel thin sheet varies significantly by material condition, the actual value requires reconfirmation against the material spec sheet. However, applying a commonly used conservative criterion (r/t ≥ 1.5, estimated), the minimum bend radius for a tab thickness of t = 0.1 mm is as follows.
$$r_{min} = 1.5 \times t = 1.5 \times 0.1\ \text{mm} = 0.15\ \text{mm}$$
The ACF area ratio is verified by directly citing the patent specification’s example. Based on a weld-rod diameter of 0.1 cm, the weld area, and, based on an ACF diameter of 0.3 cm, the total area, are as follows.
$$A_{weld} = 0.05 \times 0.05 \times \pi = 0.00785\ \mathrm{cm}^2, \quad A_{ACF} = 0.15 \times 0.15 \times \pi = 0.07065\ \mathrm{cm}^2$$
The area ratio is approximately 9x, falling within the 6–10x range presented in the specification. In equipment design, the ACF punching diameter tolerance must be managed within ±0.02 mm so as not to exceed this range.
Shop-notes
- Under consideration: Apply a bend radius of R0.2 mm (built-in safety margin) to the tab-forming die, and separate the ACF punching die into its own station to block heat effects from the welding station.
- Alternative (not adopted): An integrated head that processes ACF and welding simultaneously at one station. This reduces cycle time, but carries a risk that welding heat could affect the ACF adhesive layer, so it was not adopted pending verification data.
- Machinability note: Fine R0.2 mm-class bending depends on press-die punch edge precision (tolerance ±0.01 mm) and requires a polishing process after wire EDM.
This review does not determine whether this patent is infringed; it is an equipment-reflection review based solely on the content of the published patent gazette.
One-line summary: The ACF-reinforced tab weld structure improves adhesion at the cost of two equipment burdens: a laminating station and bend-die precision.